Why a refrigeration tube mill is different from a standard structural tube mill
A small diameter refrigeration tube is not simply a smaller structural pipe. The final product may need a clean internal surface, reliable longitudinal weld, tight outside diameter and wall thickness control, controlled mechanical properties and continuous delivery in coils.
For this reason, the production route must be designed around the application. Strip preparation, forming lubricant, weld process, reduction ratio, non-destructive testing, annealing atmosphere and coiling tension can all affect whether the finished tube is suitable for refrigeration or heat-transfer service.
A typical small diameter project definition
A buyer may request longitudinally welded steel tube with an outside diameter from about 4.00 mm to 9.52 mm, a wall thickness around 0.60 mm and delivery in continuous coils. This requirement is already more specific than a general request for an ERW tube mill, but it is not enough for final machine selection.
The engineering review should also confirm material grade, strip condition, dimensional tolerances, weld standard, internal cleanliness, required pressure or leak testing, annealed or unannealed condition, surface coating, coil diameter, coil weight and downstream tube processing.
Typical process flow for continuously coiled refrigeration tube
A complete route may include double uncoiling, strip end joining, accumulation, strip cleaning, forming a larger mother tube, longitudinal welding, outside bead removal, cooling, cold reduction to final diameter, eddy-current inspection, heat treatment when required, surface treatment and finished-tube coiling.
The exact route is project-specific. Some products may use a direct forming route, while very small final diameters may be more practical through a mother-tube and multi-pass reducing process. The final decision should follow the material, diameter range, output target and product standard.
Start from the finished tube application and quality standard
Before discussing machine speed, define where the tube will be used. Refrigeration circuits, condensers, evaporators, automotive fluid lines and general heat-transfer products can have different expectations for weld integrity, cleanliness, bendability, pressure resistance and surface protection.
Buyers should provide the applicable tube standard or an approved sample specification. If the standard is still under discussion, the inquiry should at least state the final application, working medium, pressure direction, downstream bending or end forming and required inspection method.
Continuous strip entry prevents unnecessary mill stops
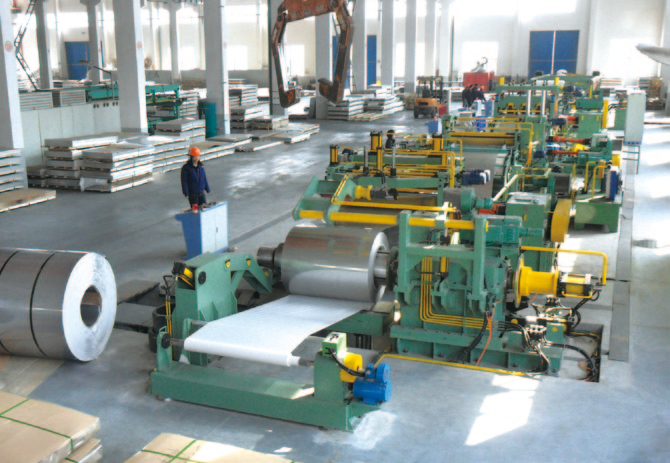
A continuous line normally needs an entry system that allows a new strip coil to be prepared while the mill keeps running. A double uncoiler, accurate strip-end cutting and joining equipment, and a correctly sized accumulator help separate coil change time from the forming and welding process.
The accumulator type and storage capacity should match strip thickness, line speed, available floor or overhead space and maintenance preference. The objective is not simply more stored strip; it is stable strip delivery without disturbing the weld and reduction sections.
Strip cleaning and internal cleanliness control
Oil, metallic particles and foreign material on the strip can become contamination inside the finished tube. A refrigeration tube project should therefore define strip surface condition and the required cleaning process before forming.
Cleaning may use brushes, controlled fluids or another method selected for the material and cleanliness target. Lubricant and cooling arrangements should also be reviewed so that forming and welding can remain stable without creating unacceptable residue inside the tube.
Why a mother-tube and cold-reduction route may be used
Producing the smallest final diameter directly at the weld station can make strip handling, weld access and internal process control difficult. One established approach is to form and weld a larger mother tube, then progressively reduce it to the required final diameter through multiple passes.
The reduction schedule should control elongation, outside diameter, wall behavior, roundness and mechanical properties. It must be engineered for the complete size range rather than selected from only the smallest requested diameter.
Selecting the longitudinal welding process
Possible welding routes for small welded tube can include high-frequency induction, contact welding, TIG or laser, depending on material, tube size, speed, cleanliness and product requirements. No single process is automatically correct for every refrigeration tube project.
High-frequency induction is a non-contact welding method, but very small tube and strict internal cleanliness requirements create special challenges around the impeder and its cooling. Contact processes avoid some impeder constraints but introduce electrode wear. TIG or laser may suit particular materials and quality targets at a different speed and cost direction. The welding route must therefore be confirmed by engineering review.
Control the weld seam before reduction
The weld seam should be stable before the tube enters the reducing section. Strip edge presentation, weld heat, squeeze condition, seam position and outside weld bead removal all influence the downstream result.
If the weld is inconsistent, later reduction can hide the visual symptom without removing the defect. Process monitoring should focus on producing a sound mother tube first, followed by controlled cooling and reduction.
Cold reduction needs synchronized drive control
During diameter reduction, the tube becomes longer and its linear speed increases. The driven passes must therefore be coordinated so each stage supports the intended reduction without excessive pulling, slipping or instability.
The number of passes, horizontal and vertical roll arrangement, drive distribution and changeover method depend on the mother-tube size, final size range, material and production speed. A quotation should explain the reduction concept rather than list only one final diameter.
Eddy-current testing and defect tracking
Online eddy-current inspection is commonly considered for detecting small discontinuities associated with the weld seam. The inspection position, calibration reference and acceptance criteria should match the applicable product standard.
For a continuously coiled product, detection alone is not enough. The control system should identify or track the affected tube length so it can be marked, separated, cut out or directed to a different coil according to the agreed quality procedure.
Annealing may be required after cold reduction
Cold reduction increases work hardening. If the finished tube needs bending, flaring, end forming or specific mechanical properties, inline or offline annealing may be required after the reducing section.
The heat-treatment method, temperature profile, protective atmosphere and cooling route depend on material grade and the required final condition. Buyers should state whether the tube must be annealed, normalized or supplied in another condition instead of treating heat treatment as a universal standard item.
Surface treatment and corrosion protection
Depending on the application, the tube may need a metallic coating, paint, oil or another surface treatment after welding and reduction. The selected coating must be compatible with later forming, joining and service conditions.
If coating is included inline, the proposal should define surface preparation, coating process, curing or cooling, quality control and how the coating affects line speed. If coating will be performed separately, the material handling route between processes should still be planned.
Finished-tube coiling is part of the production process
A tube coiler should not be treated as a simple take-up reel. It must receive the tube at a stable speed, control bending and tension, form an acceptable coil package and allow completed coils to be removed without unnecessary line stops.
Coiling design should consider minimum bending radius, tube ovality, coil inside and outside diameter, coil width, target weight or length, winding pattern, cutting method and changeover sequence. These parameters affect both tube quality and customer handling.
Coiler changeover and defective-length handling
For continuous production, a multi-station or indexed coiler arrangement can allow one finished coil to be unloaded while another is being wound. The final concept should match the expected coil size, operator method and production rate.
The line should also define what happens when the inspection system finds a defect. Options may include marking the tube, cutting out a length or indexing to another winding position. The selected method should be agreed before the automation logic is finalized.
Do not select the line by maximum speed alone
Small tube lines can reach high linear speeds, but the useful production speed depends on material, wall thickness, welding process, reduction ratio, inspection response, heat treatment, coating and coiler capability. One headline speed should not be applied to every product in the size range.
A professional proposal should provide a speed direction or production table for representative tube sizes. It should also identify which process becomes the limiting section for each product condition.
Main equipment scope to compare in quotations
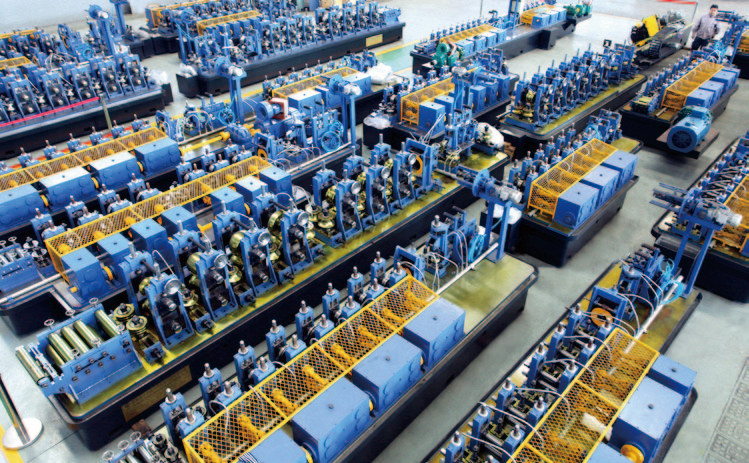
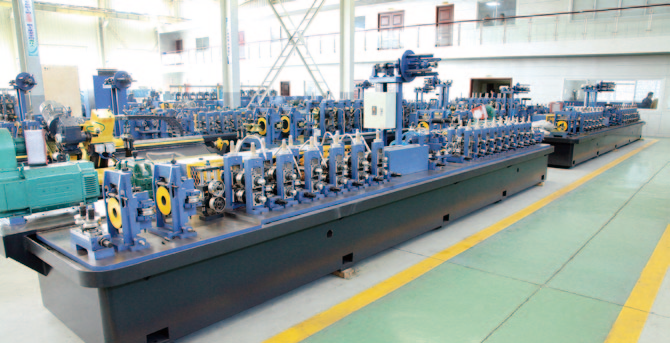
A buyer should compare the full line scope: uncoilers, strip-end joining, accumulator, cleaning, forming and welding mill, weld bead removal, cooling, reducing mill, non-destructive testing, heat treatment, surface treatment, tube coiler, electrical control and safety protection.
The quotation should identify included tooling, inspection equipment, utilities, spare parts, installation, commissioning and training. Two offers with the same title can represent very different production systems when these items are separated.
Information to send for a technical proposal
Send finished tube OD range, wall thickness range, material grade, applicable standard, tolerance, final application, welding preference if specified, target speed or annual output, required inspection, heat-treatment condition, coating and finished coil specification.
Also provide raw strip data, coil weight, workshop drawing, power and utility conditions, desired automation level and downstream processes such as bending, cutting or end forming. If a parameter is not confirmed, mark it as to be confirmed based on project requirements so the engineering team can identify the next decision.
How Zhongyue reviews a small diameter tube project
Zhangjiagang Zhongyue Metallurgy Equipment Technology Co., Ltd. can review the buyer product table, material, capacity target, quality requirements and workshop conditions before defining a proposed production route and equipment scope.
For a refrigeration tube project, the first step is to confirm whether the requested diameter, wall thickness, welding route, reduction process, inspection and coiling requirements can be integrated into a practical line. Final technical parameters and supply scope should be confirmed through project-specific engineering evaluation.
For equipment selection, visit ERW Tube Mill Line, Steel Pipe Making Machine, Direct Forming Square Tube Mill, Steel Coil Slitting Line or Tube Mill Solutions.